
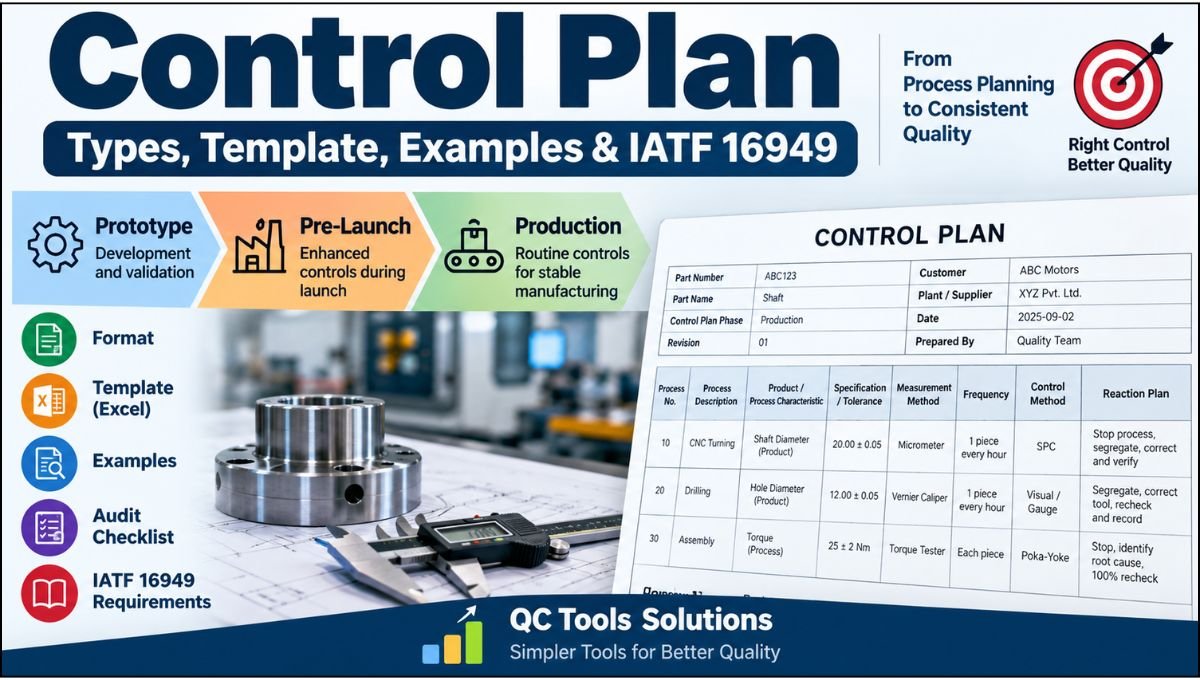
A Control Plan is a documented quality planning tool used to define how product and process characteristics will be controlled during manufacturing. It specifies what needs to be controlled, the specification or tolerance, measurement method, sample size, inspection frequency, control method and reaction plan.
In automotive manufacturing, the Control Plan is closely connected with the Process Flow Diagram, PFMEA, Special Characteristics, MSA, SPC, PPAP and IATF 16949 requirements.
A Control Plan is not simply an inspection sheet. It defines the controls needed to prevent defects, detect process problems quickly and ensure that products consistently meet customer requirements.
In this guide, you will learn:
- What is a Control Plan?
- Why is a Control Plan important?
- What are the types of Control Plans?
- How many types of Control Plans are there?
- What is a Control Plan format?
- What are the key elements of a Control Plan?
- How to prepare a Control Plan step-by-step
- What is an IATF 16949 Control Plan?
- How is a Control Plan related to PFMEA?
- Control Plan example for manufacturing
- AIAG Control Plan example
- Control Plan audit checklist
- Control Plan template in Excel
- What Is a Control Plan?
- Why is a Control Plan Important?
- Inputs required to prepare a Control Plan
- Types of Control Plans
- Control Plan Format
- Key Elements of a Control Plan
- AIAG Control Plan Example
- Example of a Control Plan in Manufacturing
- How to Prepare a Control Plan Step-by-Step
- Step 1: Review the Process Flow Diagram
- Step 2: Review the PFMEA
- Step 3: Identify Product and Process Characteristics
- Step 4: Define Specifications
- Step 5: Select the Measurement Method
- Step 6: Define Sample Size and Frequency
- Step 7: Define the Control Method
- Step 8: Develop the Reaction Plan
- Step 9: Link the Control Plan to Shop-Floor Documents
- Step 10: Review and Approve
- Step 11: Train the Relevant Personnel
- Step 12: Monitor and Update
- Relationship Between Process Flow, PFMEA and Control Plan
- Control Plan vs PFMEA
- Control Plan vs SOP vs Inspection Sheet
- IATF 16949 Control Plan Requirements
- Control Plan and PPAP
- IATF 16949 Control Plan Template
- Control Plan Audit Checklist
- When Should a Control Plan Be Updated?
- Safe Launch and the Control Plan
- Common Control Plan Mistakes
- Practical Control Plan Audit Question
- Frequently Asked Questions About Control Plans
- What is a Control Plan?
- What are the types of Control Plans?
- How many types of Control Plans are there?
- What is a Prototype Control Plan?
- What is a Pre-Launch Control Plan?
- What is a Production Control Plan?
- Is a Control Plan required by IATF 16949?
- Is the Control Plan part of PPAP?
- What is the relationship between PFMEA and Control Plan?
- What should a Control Plan contain?
- What is a Control Plan template?
- What is a Control Plan audit?
- When should a Control Plan be updated?
- Control Plan vs Inspection Plan
- Control Plan Best Practices
- Conclusion
What Is a Control Plan?
A Control Plan is a documented description of the controls used to ensure that a manufacturing process consistently produces products that meet specified requirements.
In simple words:
A Control Plan defines what to control, how to control it, how often to check it and what to do when the result is not acceptable.
A typical Control Plan identifies:
- Process operation
- Machine, equipment or tooling
- Product characteristics
- Process characteristics
- Special characteristics
- Specification and tolerance
- Measurement or testing method
- Sample size
- Inspection frequency
- Control method
- Reaction plan
- Records and responsibilities
The Control Plan should reflect actual shop-floor controls. It should therefore be practical enough for operators, quality inspectors, supervisors and process engineers to use during production.
Why is a Control Plan Important?
A Control Plan helps an organization establish consistent controls throughout the manufacturing process.
The major benefits include:
- Reducing process variation
- Preventing defects
- Detecting abnormalities at an early stage
- Defining inspection and testing requirements
- Defining process-control methods
- Establishing clear reaction plans
- Controlling special characteristics
- Supporting process capability and SPC activities
- Providing a common reference for production and quality teams
- Supporting IATF 16949 requirements
- Supporting customer-specific requirements
- Supporting PPAP activities
- Improving audit readiness
- Reducing scrap, rework and customer complaints
A good Control Plan converts the risks identified during process planning into specific controls that can be implemented on the shop floor.
Inputs required to prepare a Control Plan
A Control Plan should not be prepared independently. It should be developed using information from relevant product and process documents.
Important inputs include:
- Process Flow Diagram
- PFMEA
- DFMEA, where applicable
- Product drawing and specifications
- Customer requirements
- Special Characteristics
- Process specifications
- Work instructions and standardized work
- Inspection and testing methods
- Previous quality problems
- Process capability information
- Lessons learned
- Customer-specific requirements
The basic relationship can be understood as:
Customer Requirements → Process Flow → PFMEA → Control Plan → Work Instructions → Inspection Records
Your Process Flow Diagram article explains how the process sequence becomes an input to PFMEA and the Control Plan.
Types of Control Plans
How many types of Control Plans are there?
When discussing AIAG Control Plan phases, three main phases are commonly identified:
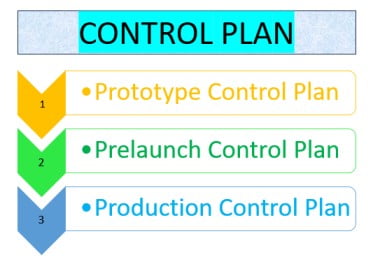
- Prototype Control Plan
- Pre-Launch Control Plan
- Production Control Plan
AIAG describes the Control Plan as a document that develops progressively through the product-development stages, including Prototype, Pre-Launch and Production. (AIAG)
These should not be confused with terms such as incoming inspection, in-process inspection and final inspection, which describe inspection or control activities rather than the three AIAG Control Plan phases.
1. Prototype Control Plan
A Prototype Control Plan is used during prototype development.
It defines the controls, measurements, tests and inspections required during prototype builds.
Typical characteristics include:
- Flexible controls
- Frequent engineering changes
- Dimensional checks
- Material verification
- Performance testing
- Prototype-specific inspection requirements
- Documentation of development findings
The Prototype Control Plan helps the organization understand how the product and process behave before moving toward production.
2. Pre-Launch Control Plan
A Pre-Launch Control Plan is used before normal production to provide additional or enhanced controls during the launch stage.
The process may still be undergoing adjustment, validation and stabilization, so additional inspection or containment may be appropriate based on risk.
Typical controls may include:
- Increased inspection frequency
- Additional dimensional checks
- Additional process monitoring
- Enhanced testing
- Additional error-proofing verification
- Additional containment
- Increased management review
The exact requirements should be determined by the organization, customer requirements and applicable customer-specific requirements.
3. Production Control Plan
A Production Control Plan is used during normal production.
It defines the routine controls required to maintain consistent product and process quality.
Typical controls include:
- Process parameters
- Product characteristics
- Special characteristics
- Inspection frequency
- Measurement methods
- SPC
- Error-proofing
- Preventive controls
- Reaction plans
- Process monitoring
The Production Control Plan should be based on the actual production process and updated when significant changes or quality issues occur.
Prototype vs Pre-Launch vs Production Control Plan
| Control Plan | Main Purpose | Typical Stage |
|---|---|---|
| Prototype | Control prototype builds and development activities | Product development |
| Pre-Launch | Provide enhanced controls during launch | Before/around production launch |
| Production | Control the established production process | Regular production |
Control Plan Format
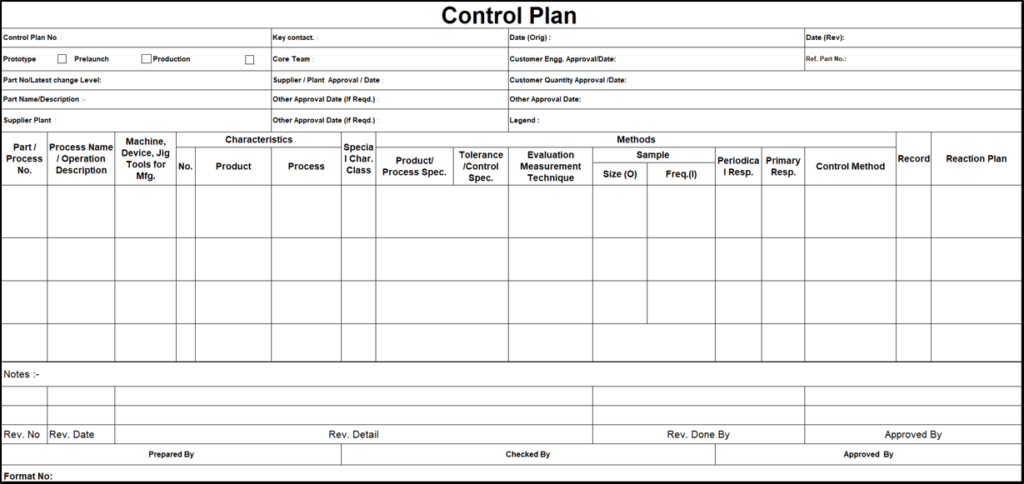
A Control Plan format normally contains two major parts:
Control Plan Header
The header generally contains information such as:
- Control Plan number
- Part number
- Part name
- Revision level
- Control Plan phase
- Customer name
- Supplier/plant name
- Key contact
- Core team
- Date
- Approval information
- Process reference
Control Plan Body
The body defines the actual product and process controls.
Typical information includes:
- Process number
- Process description
- Machine/equipment/tool
- Product characteristic
- Process characteristic
- Special characteristic
- Specification/tolerance
- Measurement technique
- Sample size
- Frequency
- Control method
- Reaction plan
- Record/reference
The exact format may vary according to the customer, industry and applicable Control Plan manual.
Key Elements of a Control Plan
A practical Control Plan should answer five basic questions:
What? → Where? → How? → How often? → What if it fails?
Important elements include:
1. Process Number
Identifies the operation according to the Process Flow Diagram.
2. Process Description
Describes the manufacturing or inspection operation.
3. Machine, Device or Tool
Identifies the equipment, machine, fixture, jig, gauge or tooling used.
4. Product Characteristic
Identifies the characteristic of the product that needs to be controlled.
Example:
Shaft diameter = 20.00 ± 0.05 mm
5. Process Characteristic
Identifies a process parameter that affects product quality.
Examples:
- Welding current
- Welding time
- Torque
- Temperature
- Pressure
- Speed
- Feed rate
6. Special Characteristics
Special characteristics identified by the customer or organization should be appropriately identified and controlled.
7. Specification/Tolerance
The applicable drawing, specification or process requirement is defined.
8. Measurement Technique
Defines how the characteristic will be measured.
Examples:
- Vernier caliper
- Micrometer
- Bore gauge
- Height gauge
- CMM
- Torque tester
- Visual inspection
- Functional test
9. Sample Size
Defines how many pieces or measurements are to be checked.
10. Inspection Frequency
Defines when the inspection is performed.
Examples:
- First piece
- Every hour
- Every 2 hours
- Every batch
- Start/middle/end of shift
- 100% inspection
Frequency should be based on risk, process performance, customer requirements and applicable specifications.
11. Control Method
Defines how the process is controlled.
Examples:
- SPC
- Error-proofing
- Parameter monitoring
- Setup verification
- Visual inspection
- Automatic detection
- Preventive control
12. Reaction Plan
Defines what must happen when a nonconforming condition or abnormal process condition is detected.
A good reaction plan should identify actions such as:
- Stop the process
- Identify and segregate suspect product
- Inform the responsible person
- Correct the process
- Verify the correction
- Reinspect affected product
- Record the result
- Restart production only after defined acceptance criteria are met
AIAG Control Plan Example
Consider a CNC turning process.
Example: Shaft Diameter Control
| Control Plan Item | Example |
|---|---|
| Process | CNC Turning |
| Machine | CNC Lathe |
| Characteristic | Shaft Diameter |
| Specification | 20.00 ± 0.05 mm |
| Special Characteristic | As applicable |
| Measurement Method | Micrometer |
| Sample Size | 1 piece |
| Frequency | Every 1 hour |
| Control Method | SPC / process parameter control |
| Reaction Plan | Stop process, segregate suspect parts, correct process and verify |
This example shows the basic logic of a Control Plan.
The Control Plan should not simply say:
“Check diameter.”
It should tell the operator or inspector:
What diameter? What specification? With which instrument? How many pieces? At what frequency? What should be done if the result is out of specification?
That is what makes a Control Plan effective.
Example of a Control Plan in Manufacturing
Consider a drilling operation.
Process: Drilling
Machine: Radial Drill
Characteristic: Hole diameter
Specification: 12.00 ± 0.05 mm
Measurement: Vernier/calibrated gauge as appropriate to the required accuracy
Frequency: 1 piece every hour
Control: Tool setting and periodic verification
Reaction: Stop process, segregate suspect production, investigate tool/process condition, correct the process and verify conformity before restart.
The actual measurement equipment and sampling frequency must be appropriate for the tolerance, risk and customer requirements.
How to Prepare a Control Plan Step-by-Step
Step 1: Review the Process Flow Diagram
Start with the actual process sequence.
Make sure all manufacturing, inspection, testing, rework and relevant material-flow steps are considered.
You can refer to our Process Flow Diagram guide.
Step 2: Review the PFMEA
Identify the process failure modes and controls identified in the PFMEA.
The Control Plan should reflect the appropriate controls resulting from the process-risk analysis.
For more information, see our PFMEA guide.
Step 3: Identify Product and Process Characteristics
List the characteristics that need to be controlled.
These can include:
- Dimensions
- Material
- Appearance
- Performance
- Process parameters
- Functional characteristics
- Special characteristics
Step 4: Define Specifications
Enter the correct drawing, customer or process specification.
Never copy tolerances from an old Control Plan without verifying the current drawing revision.
Step 5: Select the Measurement Method
Select an appropriate measurement or test method.
The measurement system should be suitable for the characteristic and its tolerance.
Where required, MSA should be considered.
Step 6: Define Sample Size and Frequency
Determine:
- How many parts to inspect?
- How frequently?
- Who will inspect?
- What records are required?
Sampling should be based on risk, process performance, customer requirements and applicable requirements.
Step 7: Define the Control Method
Decide how the process will actually be controlled.
A preventive control is generally preferable to relying only on final inspection.
Step 8: Develop the Reaction Plan
Clearly define what happens when:
- Product is out of specification
- Process becomes unstable
- Process becomes incapable
- Error-proofing fails
- A special characteristic is not controlled
- An abnormal condition occurs
Step 9: Link the Control Plan to Shop-Floor Documents
The Control Plan should be consistent with:
- Work instructions
- SOPs
- Inspection standards
- Check sheets
- Setup instructions
- Testing procedures
Step 10: Review and Approve
Review the Control Plan with appropriate functions such as:
- Quality
- Production
- Process Engineering
- Manufacturing Engineering
- Maintenance, where relevant
Customer approval should be obtained when required by the applicable customer requirements.
Step 11: Train the Relevant Personnel
Operators and inspectors should understand the controls that apply to their operations.
Step 12: Monitor and Update
The Control Plan is a living document.
It should be reviewed and updated when changes, quality problems, customer complaints, process risks or other defined triggers require an update.
Relationship Between Process Flow, PFMEA and Control Plan
One of the most important concepts in automotive quality is the relationship:
Process Flow → PFMEA → Control Plan
The Process Flow tells us:
What happens?
PFMEA asks:
What can go wrong?
Control Plan defines:
How will we control it?
For example:
Process: Tightening
PFMEA failure mode: Insufficient torque
Control Plan: Torque value controlled using a calibrated torque tool, with defined verification frequency and reaction plan.
Therefore:
PFMEA identifies process risk, while the Control Plan translates appropriate controls into shop-floor execution.
AIAG also describes the Control Plan as an integral part of APQP and as a living document that evolves with improvements and lessons learned. (AIAG)
Control Plan vs PFMEA
| PFMEA | Control Plan |
|---|---|
| Identifies potential process failures | Defines controls for those risks |
| Focuses on risk analysis | Focuses on process control |
| Identifies causes and effects | Defines measurement and control methods |
| Evaluates risk | Establishes operational controls |
| Recommends actions | Implements controls on the shop floor |
A simple way to remember this is:
PFMEA = What can go wrong?
Control Plan = How will we control it?
Control Plan vs SOP vs Inspection Sheet
These documents have different purposes.
| Document | Main Purpose |
|---|---|
| Control Plan | Defines what to control, how, frequency and reaction |
| SOP/Work Instruction | Defines how the operation should be performed |
| Inspection Sheet | Records actual inspection results |
| PFMEA | Identifies and evaluates process risks |
A Control Plan does not replace the SOP or Work Instruction.
Instead, these documents should work together.
IATF 16949 Control Plan Requirements
Control Plan requirements are addressed in IATF 16949:2016 Clause 8.5.1.1 – Control Plan. IATF’s published information continues to identify IATF 16949:2016 as the applicable standard edition, with the latest related interpretations and customer-specific requirements maintained separately. (IATF Global Oversight)
Clause 8.5.1.1 requires organizations to establish Control Plans for the relevant manufacturing scope and requires linkage with relevant risk-analysis and process-planning information.
Important areas include:
- Pre-launch and production Control Plans
- Linkage with Process Flow
- Linkage with manufacturing process risk analysis such as PFMEA
- Manufacturing process controls
- Verification of job setups
- First-off/last-off validation where applicable
- Control of special characteristics
- Customer-required information
- Reaction plans
- Review and updating of the Control Plan
The Control Plan should therefore not be treated as an independent quality document.
It should be consistent with the actual process and the related quality-planning documents.
IATF also emphasizes the relationship between Control Plans, PFMEA updates and process controls. AIAG’s overview of IATF 16949 highlights these linkages and the importance of keeping the Control Plan aligned with changes and risk analysis.
Control Plan and PPAP
The Control Plan is one of the important documents associated with automotive PPAP activities.
It provides evidence that the organization has defined how the product and process will be controlled during production.
However, PPAP submission requirements are customer-specific. The customer determines the required submission level and supporting documentation.
Therefore, it is better to say:
The Control Plan supports PPAP by demonstrating the planned controls for product and process conformity. The exact PPAP submission requirements depend on the customer and applicable requirements.
For a detailed explanation, see our PPAP Process guide.
IATF 16949 Control Plan Template
If you are looking for an IATF 16949 Control Plan template, the template should contain enough information to define the manufacturing controls clearly.
A practical Control Plan template normally includes:
Header:
- Control Plan number
- Part number
- Part name
- Revision
- Customer
- Supplier/plant
- Control Plan phase
- Core team
- Dates and approvals
Body:
- Process number
- Process description
- Machine/tool
- Product characteristic
- Process characteristic
- Special characteristic
- Specification/tolerance
- Measurement technique
- Sample size
- Frequency
- Control method
- Reaction plan
- Record/reference
Download Control Plan Format in Excel
You can provide your existing Control Plan Excel template here.
Download Control Plan Format in Excel
Control Plan Audit Checklist
A Control Plan audit should verify not only the document but also whether the documented controls are actually implemented on the shop floor.
Document Review
- Is the latest Control Plan revision available?
- Is the correct part number mentioned?
- Is the correct drawing revision referenced?
- Is the Control Plan approved?
- Is the applicable Control Plan phase identified?
- Are customer requirements included?
Process Review
- Does the Control Plan match the actual Process Flow?
- Does it cover all applicable process operations?
- Does it match the PFMEA?
- Are special characteristics identified?
- Are product characteristics correctly specified?
- Are process characteristics correctly identified?
Measurement Review
- Is the correct measurement method specified?
- Is the measuring equipment suitable?
- Is the measuring equipment calibrated where required?
- Is sample size defined?
- Is inspection frequency defined?
- Are SPC or other statistical controls used where required?
Reaction Plan Review
- Is the reaction plan clearly defined?
- Does it specify containment?
- Does it identify what happens to suspect product?
- Does it define process correction?
- Does it define verification before restart?
- Are records maintained?
Shop-Floor Verification
Ask:
“Show me how you control this characteristic.”
Then compare:
Control Plan → Work Instruction → Actual Process → Inspection Record
All four should be consistent.
IATF-related guidance also emphasizes the value of comparing the approved Control Plan with the controls actually applied in manufacturing.
When Should a Control Plan Be Updated?
A Control Plan should be reviewed and updated when applicable changes or quality events occur.
Examples include:
- Engineering changes
- Drawing revisions
- Process changes
- Machine or tooling changes
- Measurement-method changes
- Supplier/source changes
- Production-volume changes
- PFMEA changes
- Customer complaints
- Nonconforming product
- Corrective actions
- Changes in process risk
- Lessons learned
- Customer-specific requirements
IATF 16949 Clause 8.5.1.1 includes defined triggers for reviewing and updating Control Plans, including changes affecting the product, manufacturing process, measurement, logistics, supply sources, production volume or FMEA, as well as customer complaints and other risk-based review requirements.
Safe Launch and the Control Plan
Modern automotive Control Plan practices also place greater emphasis on Safe Launch.
AIAG’s current Control Plan material identifies Safe Launch as an important part of the updated Control Plan approach, particularly around launch and enhanced controls.
Safe Launch can involve temporary additional controls or containment intended to protect the customer while the new or changed process demonstrates stable performance.
The organization should define:
- Additional launch controls
- Duration or exit criteria
- Responsibilities
- Data collection
- Escalation
- Conditions for returning to normal production controls
Customer-specific requirements may establish additional Safe Launch expectations.
For example, IATF’s published OEM requirements show that customer-specific requirements can add specific Control Plan expectations. (IATF Global Oversight)
Common Control Plan Mistakes
Some common mistakes include:
- Copying an old Control Plan without reviewing the current process
- Not linking the Control Plan with PFMEA
- Missing process steps
- Missing special characteristics
- Incorrect drawing revision
- Undefined inspection frequency
- Undefined sample size
- Weak reaction plans
- Relying only on final inspection
- Ignoring process parameters
- Not updating the Control Plan after changes
- Not training operators
- Having controls in the Control Plan that are not actually performed
- Having shop-floor controls that are missing from the Control Plan
The most serious problem is often the gap between the documented Control Plan and actual shop-floor practice.
Practical Control Plan Audit Question
During an audit, ask the operator:
“What do you check at this operation?”
Then ask:
“What is the specification?”
“How do you check it?”
“How frequently do you check it?”
“What will you do if the result is not OK?”
The answers should match the Control Plan and applicable work instructions.
This is a simple but powerful way to verify Control Plan effectiveness.
Frequently Asked Questions About Control Plans
What is a Control Plan?
A Control Plan is a documented plan that defines product and process characteristics, specifications, measurement methods, frequencies, control methods and reaction plans used to maintain product and process conformity.
What are the types of Control Plans?
The commonly recognized AIAG Control Plan phases are:
- Prototype
- Pre-Launch
- Production
How many types of Control Plans are there?
For the AIAG Control Plan phases, there are three commonly recognized phases: Prototype, Pre-Launch and Production.
What is a Prototype Control Plan?
It defines the controls, measurements and tests used during prototype development.
What is a Pre-Launch Control Plan?
It defines the controls used during the pre-launch stage, often with additional or enhanced controls while the process is being prepared for regular production.
What is a Production Control Plan?
It defines the routine product and process controls used during normal production.
Is a Control Plan required by IATF 16949?
Yes. IATF 16949 Clause 8.5.1.1 contains requirements for Control Plans, including pre-launch and production Control Plans and their linkage with relevant process and risk-analysis information. (IATF Global Oversight)
Is the Control Plan part of PPAP?
The Control Plan is an important document supporting PPAP and production approval activities. However, the exact PPAP submission requirements depend on the customer and applicable customer-specific requirements.
What is the relationship between PFMEA and Control Plan?
PFMEA identifies and evaluates process risks, while the Control Plan defines the controls used to manage those risks.
What should a Control Plan contain?
It should normally include process steps, characteristics, specifications, measurement methods, sample size, frequency, control methods and reaction plans, together with applicable header and approval information.
What is a Control Plan template?
A Control Plan template is a structured format used to document product and process controls. It can be maintained in Excel or another controlled document format.
What is a Control Plan audit?
A Control Plan audit verifies whether the documented controls are suitable, current and actually implemented on the shop floor.
When should a Control Plan be updated?
It should be updated when relevant changes, quality problems, customer complaints, PFMEA changes, process changes or other defined review triggers affect the control strategy.
Control Plan vs Inspection Plan
A Control Plan is broader than an inspection plan.
An inspection plan mainly focuses on inspection activities.
A Control Plan can include:
- Prevention controls
- Process parameters
- Error-proofing
- Setup verification
- Product inspection
- Process monitoring
- Special-characteristic controls
- Reaction plans
Therefore:
Inspection is one part of process control; a Control Plan defines the overall control strategy.
Control Plan Best Practices
For an effective Control Plan:
- Keep it simple and practical.
- Link it to the Process Flow.
- Link it to PFMEA.
- Include all applicable special characteristics.
- Use current drawing and specification revisions.
- Define realistic inspection frequencies.
- Use appropriate measurement methods.
- Include preventive controls.
- Make reaction plans specific.
- Train operators and inspectors.
- Verify implementation through audits.
- Update the Control Plan after relevant changes.
- Consider customer-specific requirements.
- Use lessons learned from previous problems.
The Control Plan should be a living document, not a document prepared only for an audit or PPAP submission.
Conclusion
A Control Plan is one of the most important quality-control documents in manufacturing. It converts process risks and customer requirements into practical controls that can be implemented on the shop floor.
The most important relationship to remember is:
Process Flow → PFMEA → Control Plan → Work Instruction → Inspection Record
The Control Plan should define:
What to control → Specification → How to measure → Frequency → Control method → Reaction plan
For automotive organizations, the Control Plan also plays an important role in meeting IATF 16949 requirements, customer-specific requirements and PPAP expectations.
A well-prepared Control Plan can help reduce process variation, prevent defects, improve audit readiness and ensure that the manufacturing process consistently produces conforming products.
For organizations using the current AIAG approach, it is also important to consider the updated Control Plan guidance and Safe Launch expectations, together with the applicable customer-specific requirements.
This sample shows how a Control Plan clearly defines what needs to be controlled and how.
Hi, you have shared a good information. My query is whether this can be followed by sales and service industry too?
Thank you.
Thanks for your query.These control plans are for the manufacturing industry only. But control plan for service industry can be created.
I highly recommend ernestopro.com for anyone looking to implement effective control plans in quality management. Their comprehensive approach and detailed resources on different types of control plans, including IATF 16949 standards, make them an invaluable partner. The clarity in their format examples and input guidelines greatly simplify the process of preparing and understanding control plans. Trust ernestopro.com to enhance your quality control processes with expert support and insightful solutions.
Fabulous, what a blog it is! This weblog provides valuable
facts to us, keep it up.
What’s up Dear, are you really visiting this web page daily, if so then you will without doubt take nice
know-how.
Write more, thats all I have to say. Literally, it seems as though you relied on the video to make your point.
You definitely know what youre talking about, why waste your intelligence on just posting videos to your site when you could be giving us
something enlightening to read?
Hey there! I simply would like to offer you a big thumbs
up for the great information you have here on this post.
I’ll be coming back to your website for more soon.
I do consider all the ideas you’ve offered on your post.
They are really convincing and can certainly work.
Still, the posts are very short for newbies. Could you please lengthen them
a bit from next time? Thanks for the post.
My brother suggested I may like this web site. He was once totally right.
This put up actually made my day. You cann’t consider just how much time I had spent for this info!
Thank you!
Please let me know if you’re looking for a article author for your blog.
You have some really great articles and I think I would be a good asset.
Hiya, I’m really glad I’ve found this information. Today bloggers publish just about gossips and internet and this is really irritating. A good web site with interesting content, this is what I need. Thanks for keeping this website, I will be visiting it. Do you do newsletters? Can’t find it.
I gotta favorite this site it seems very beneficial.
I am actually glad to read this web site posts which carries lots of valuable facts, thanks for providing such
data.