
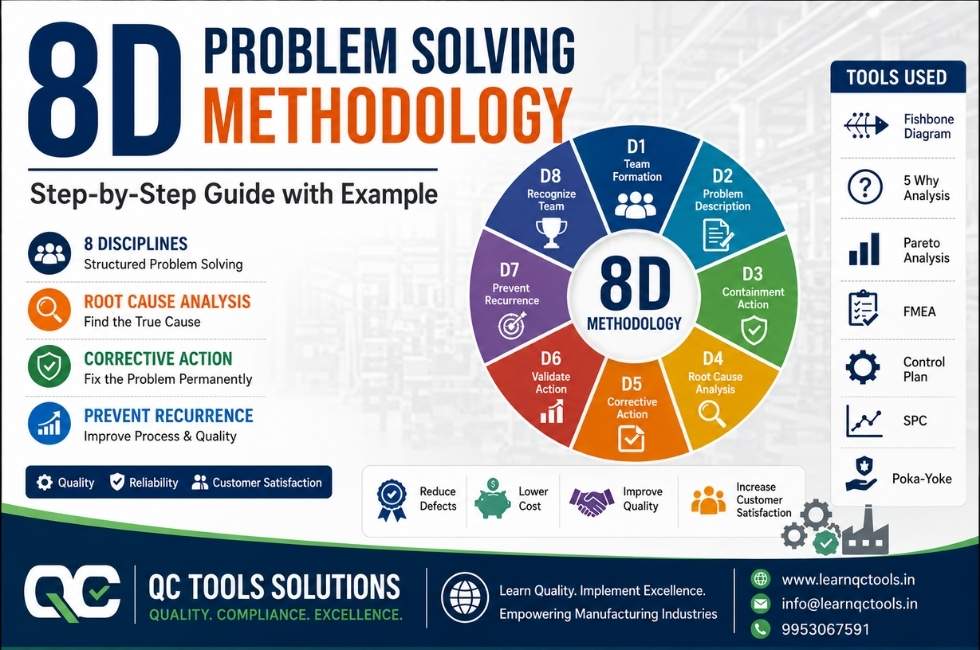
8D Problem Solving is a structured methodology used by quality engineers and cross-functional teams to investigate customer complaints, process defects, and recurring manufacturing problems. It helps organizations contain the immediate issue, identify verified root causes, implement permanent corrective actions, and prevent recurrence.
In this guide, you will learn all eight disciplines of 8D, practical manufacturing examples, root cause analysis tools, and how to prepare an effective 8D report.
In this detailed guide, you will learn:
- What is 8D problem solving
- Why 8D is important in manufacturing
- 8D methodology steps explained
- Real manufacturing example
- Tools used in 8D
- Difference between 8D and CAPA
- Common mistakes in 8D reports
- Practical tips for implementation
What is 8D Problem Solving?
8D stands for Eight Disciplines Problem Solving. It is a systematic approach used to identify, correct, and eliminate recurring problems.
The 8D method was originally developed by the automotive industry (Ford Motor) and later became a standard problem-solving technique across manufacturing sectors.
Primary objectives of 8D methodology:
- Identify root cause
- Implement corrective action
- Prevent recurrence
- Improve customer satisfaction
- Strengthen manufacturing processes
The 8D process is commonly used for:
- Customer complaints
- Supplier quality issues
- Field failures
- Warranty claims
- Repetitive defects
- Safety problems
- Process failures
Why 8D Problem Solving is important in manufacturing?
Manufacturing companies deal with quality issues daily. If problems are solved only temporarily, defects will repeat. The 8D methodology focuses on permanent corrective action instead of short-term fixes.
Benefits of 8D methodology:
- Reduces customer complaints
- Improves product quality
- Eliminates recurring defects
- Enhances supplier quality performance
- Improves team collaboration
- Supports IATF 16949 compliance
- Strengthens root cause analysis
- Reduces cost of poor quality (COPQ)
Automotive OEMs and Tier-1 suppliers often demand 8D reports from suppliers for customer complaints and field failures.
8 Steps of 8D Problem Solving Methodology
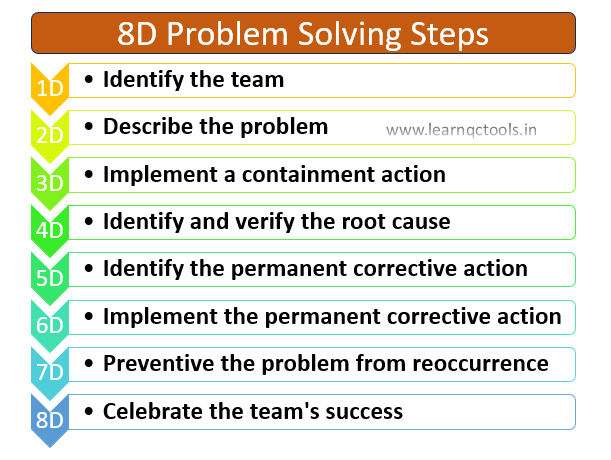
The 8D process contains eight structured disciplines.
| 8D Step | Purpose | Common Tools |
|---|---|---|
| D1 | Establish Team | Cross-functional team |
| D2 | Describe Problem | 5W2H, Is/Is Not |
| D3 | Implement Containment | Segregation, Sorting |
| D4 | Identify Root Cause | Fishbone, 5 Whys |
| D5 | Choose Corrective Action | Verification |
| D6 | Validate Corrective Action | Monitoring |
| D7 | Prevent Recurrence | FMEA, Control Plan |
| D8 | Recognize Team | Lessons Learned |
D1 – Establish the Team
The first step is to form a cross-functional team with knowledge of the process and product.
The team may include:
- Quality engineer
- Production engineer
- Maintenance engineer
- Supplier quality engineer
- Process owner
- Operator
A strong team ensures better root cause analysis and faster implementation.
D2 – Describe the Problem
The problem should be clearly defined using measurable data.
Most companies use:
- 5W2H
- Is/Is Not analysis
- Defect photographs
- Customer complaint details
Example:
- What: Scratch mark on component
- Where: Final inspection
- When: Night shift
- How many: 120 parts
- Customer impact: Line stoppage
A poorly defined problem leads to incorrect corrective action.
D3 – Implement Containment Action
Containment action protects the customer until permanent corrective action is implemented.
Typical containment actions:
- 100% inspection
- Sorting
- Rework
- Line stoppage
- Stock segregation
- Customer stock inspection
Containment action should be immediate and effective.
D4 – Identify Root Cause
This is the most critical step of the 8D process.
The objective is to identify:
- Root cause of occurrence
- Root cause of escape (Outflow)
Common root cause analysis tools:
- 5 Why Analysis
- Fishbone Diagram
- Pareto Analysis
- Process Mapping (VSM)
Example:
Problem: Missing clip in assembly
Why 1: Clip not fitted
Why 2: Sensor did not detect missing clip
Why 3: Sensor bypassed during maintenance
Why 4: No validation after maintenance
Why 5: SOP missing verification step
Root cause:
Maintenance verification process was inadequate.
D5 – Choose Permanent Corrective Action
After identifying the root cause, the team selects permanent corrective actions.
Corrective actions should:
- Eliminate root cause
- Be practical
- Be measurable
- Prevent recurrence
Examples:
- Install poka-yoke system (error-proofing)
- Update SOP
- Add sensor interlock
- Modify fixture design
The team should verify whether corrective actions will actually eliminate the problem.
D6 – Implement and Validate Corrective Action
Corrective actions are implemented and monitored for effectiveness.
Validation activities may include:
- Process audits
- Customer feedback
- Defect trend analysis
- SPC monitoring
- Layered process audits
The company must ensure the defect does not recur.
D7 – Prevent Recurrence
This step ensures the same problem does not appear in other products or processes.
Typical preventive actions:
- Update FMEA
- Revise Control Plan
- Update SOPs
- Update other relevant documents like Check sheets, inspection standards, WI etc
- Provide training
This step is extremely important in IATF 16949 systems.
D8 – Recognize the Team
The final step is to appreciate team efforts and document lessons learned.
Recognition improves:
- Team motivation
- Employee engagement
- Problem-solving culture
Lessons learned should be shared across departments.
Real Manufacturing Example of 8D Problem Solving
Customer Complaint Example in Automotive Industry
Problem
Customer reported missing clips in dashboard assembly.
D1 Team Formation
Cross-functional team formed with quality, production, and maintenance departments.
D2 Problem Description
- Defect: Missing clip
- Quantity: 45 vehicles
- Shift: Night shift
- Customer impact: Assembly line stoppage
D3 Containment Action
- 100% inspection started
- Customer stock checked
- Suspected batches isolated
D4 Root Cause Analysis
Root cause identified:
Sensor bypassed during preventive maintenance.
Escape point:
Layered process audit failed to verify sensor condition.
D5 Permanent Corrective Action
- Interlock system added
- Sensor validation checklist introduced
- Maintenance SOP updated
D6 Validation
No defect observed for 3 months.
D7 Prevention
- PFMEA updated
- Control Plan revised
- Training conducted
D8 Recognition
Team appreciated during monthly quality meeting.
Tools Used in 8D Problem Solving
Several quality tools support effective 8D implementation.
1. Fishbone Diagram
Used for identifying possible causes. (Cause & Effect Diagram)
2. 5 Why Analysis
Used for deep root cause analysis.
3. Pareto Analysis
Helps identify major defect contributors.
4. FMEA
Prevents future failures.
5. Control Plan
Defines process controls.
6. SPC
Monitors process performance.
7. Poka-Yoke
Prevents human errors.
Difference Between 8D and CAPA
| Parameter | 8D | CAPA |
|---|---|---|
| Focus | Problem solving | System improvement |
| Structure | 8 disciplines | Corrective & preventive action |
| Industry Use | Automotive | All industries |
| Team Approach | Strongly team-based | May be individual |
| Root Cause Depth | Very detailed | Moderate |
| Customer Complaint Use | Common | Common |
8D is more structured and detailed compared to traditional CAPA systems.
8D vs A3 Problem Solving
| Feature | 8D | A3 |
|---|---|---|
| Origin | Automotive | Toyota |
| Documentation | Detailed | One-page |
| Best For | Complex problems | Lean improvement |
| Customer Requirement | Frequently used | Less common |
Common mistakes in 8D Reports
Many companies fail to implement effective 8D methodology due to these mistakes:
- Weak problem definition
- Poor containment action
- Incorrect root cause analysis
- Blaming operators only
- No validation of corrective action
- Failure to update FMEA
- Lack of management involvement
The most common mistake is confusing symptom with root cause.
How 8D Supports IATF 16949
IATF 16949 strongly emphasizes:
- Problem solving
- Root cause analysis
- Corrective action
- Risk reduction
- Customer complaint management
8D methodology supports compliance with:
- Clause 10.2 Corrective Action
- Customer-specific requirements
- Supplier corrective action requests (SCAR)
Most automotive customers require suppliers to submit 8D reports within defined timelines.
Best Practices for Effective 8D Implementation
To make 8D successful:
- Use cross-functional teams (CFT)
- Focus on data-based analysis
- Verify root cause properly
- Implement mistake-proofing
- Update quality documents
- Monitor effectiveness
- Train employees regularly
Strong management support is also essential.
Free 8D PDF Format
8D Excel Format
Frequently Asked Questions (FAQs)
What is 8D problem solving?
8D is a structured, team-based approach for investigating quality problems, implementing corrective actions, and preventing recurrence.
What are the 8 steps of 8D?
The eight disciplines cover team formation, problem description, containment, root cause, permanent corrective action, validation, recurrence prevention, and team recognition.
What is the difference between containment and corrective action?
Containment protects the customer or process from the immediate problem, while permanent corrective action addresses the verified cause and is validated for effectiveness.
What tools are used in 8D problem solving?
Common tools include 5 Whys, Fishbone diagrams, Pareto analysis, FMEA, Control Plan, and SPC, selected according to the problem and evidence required.
What is the purpose of an 8D report?
An 8D report documents the complete problem-solving process, including containment, root cause analysis, corrective action, and prevention.
What is containment action in 8D?
Containment action is a temporary action taken to protect the customer from defective products until permanent corrective action is implemented.
What is the difference between CAPA and 8D?
CAPA is a broader corrective action system, while 8D is a detailed team-based problem-solving methodology commonly used in automotive industries.
Conclusion
8D Problem Solving Methodology is an effective, structured approach for identifying root causes, implementing corrective actions, and preventing recurring quality problems. By applying all eight disciplines with tools such as 5 Why, Fishbone Diagram, and FMEA, organizations can improve product quality, customer satisfaction, and process performance. A properly prepared 8D report promotes teamwork, systematic problem-solving, and continuous improvement in manufacturing and other industries.
Need support for 8D problem solving, customer complaint handling, supplier quality improvement, IATF 16949 audits, or root cause analysis implementation? QC Tools Solutions provides consultancy support for manufacturing industries & provide online QMS training.
This is a great resource. Thank you for sharing.