
Value Added vs. Non-Value-Added Activities in Manufacturing: Examples, Differences and Improvement
In manufacturing, every activity consumes time, manpower, equipment, energy and other resources. However, not every activity contributes directly to the value of the final product from the customer’s perspective.
Value Added (VA) and Non-Value Added (NVA) activities are important concepts in Lean Manufacturing and process improvement. Identifying these activities helps organizations reduce waste, improve productivity, shorten lead time, reduce manufacturing costs and increase customer satisfaction.
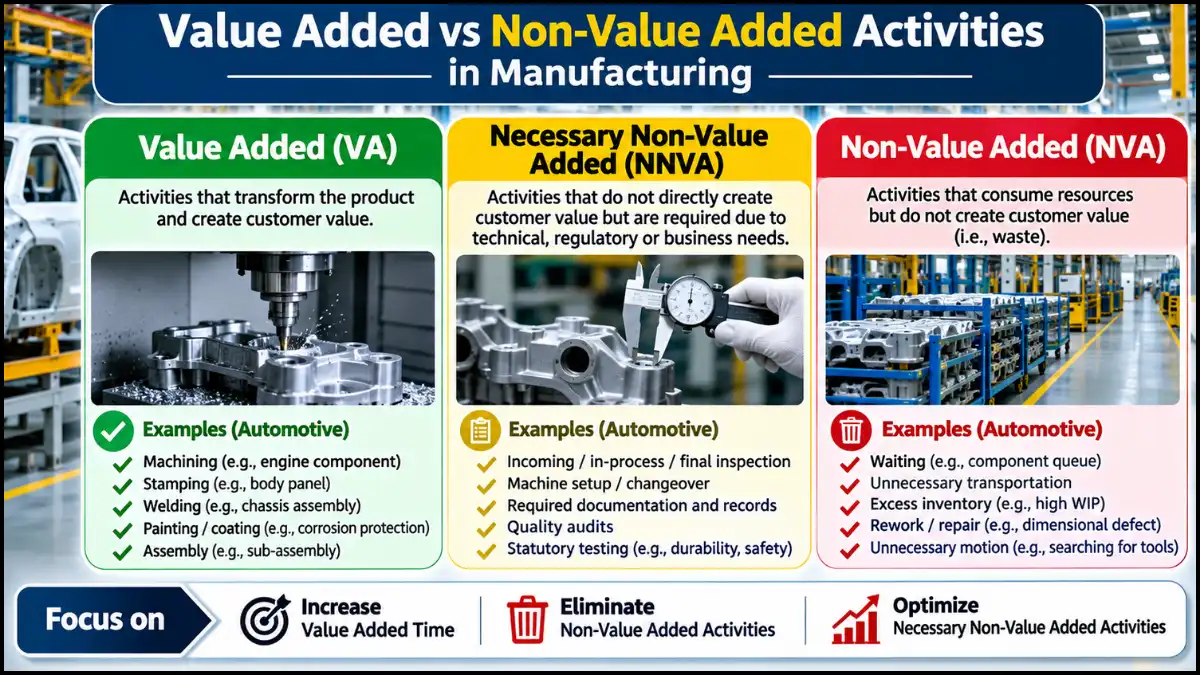
In the automotive industry, activities such as machining, stamping, welding, painting and assembly transform raw materials into finished components. These are generally value-added activities when they meet customer requirements and are performed the first time correctly.
On the other hand, waiting, unnecessary transportation, excess inventory, rework and unnecessary movement are examples of non-value-added activities.
Some activities, such as inspection, documentation and machine setup, may not directly add value but are necessary under current technical, regulatory or audit requirements. These are commonly classified as Necessary Non-Value Added (NNVA) activities.
In this article, we will understand the difference between value-added, non-value-added and necessary non-value-added activities with practical automotive manufacturing examples, comparison tables, calculations and Lean improvement techniques.
Table of Contents
- What Are Value Added Activities?
- Three Criteria of Value Added Activities
- Examples of Value Added Activities in Manufacturing
- What Are Non-Value Added Activities?
- Examples of Non-Value Added Activities
- What Are Necessary Non-Value Added Activities?
- Difference Between VA, NVA and NNVA Activities
- Value Added vs Non-Value Added Activities in Automotive Manufacturing
- Relationship Between Non-Value Added Activities and the 8 Wastes
- Value Added Time, Non-Value Added Time and Process Cycle Efficiency
- How to Identify Non-Value Added Activities
- How to Eliminate Non-Value Added Activities
- Benefits of Reducing Non-Value Added Activities
- Application in ISO 9001 and IATF 16949
- Frequently Asked Questions
- Conclusion
1. What Are Value Added Activities?
A Value Added Activity (VA) is an activity or process step that transforms a product or service in a way that creates value for the customer.
In simple words, value-added activities are those activities for which the customer recognizes value and is willing to pay.
In manufacturing, these activities change the form, fit, function or characteristics of a product according to customer requirements.
For example, when a steel component undergoes machining, its dimensions and shape are changed to meet the drawing specifications. This machining operation creates value because it transforms the raw material into a required component.
Similarly, welding, stamping, painting, heat treatment and assembly can be value-added activities when they fulfil the required customer specifications.
Value-added activities are important because they directly contribute to delivering the product or service that the customer expects.
2. Three Criteria of Value-Added Activities
According to the commonly used Lean Manufacturing approach, an activity should satisfy three criteria to be classified as value-added.
1. Customer Must Be Willing to Pay
The activity must contribute to something that the customer values.
For example, a customer purchasing an automotive shaft expects the shaft to have the specified diameter, length and surface finish.
Therefore, the machining operations that produce these characteristics contribute to customer value.
2. Product or Service Must Be Transformed
The activity must change the form, fit, function or characteristics of the product or deliver the intended service outcome.
Examples:
- Cutting steel sheets into required shapes.
- Machining a component to specified dimensions.
- Welding two components together.
- Painting a product to the specified coating requirements.
- Assembling different components into a finished product.
3. Activity Must Be Done Right First Time
The activity must be performed correctly without requiring rework or repair.
For example, if a component is machined correctly according to the drawing specifications, it is a value-added operation.
However, if the component requires additional machining because of an incorrect operation, that additional work is rework and is considered non-value-added.
Remember: An activity should satisfy all three criteria to be classified as value-added.
3. Examples of Value-Added Activities in Manufacturing
The following are practical examples of value-added activities in automotive and engineering manufacturing.
| Manufacturing activity | Why it adds value |
|---|---|
| Stamping | Forms sheet metal into the required shape |
| CNC machining | Produces required dimensions and geometry |
| Welding | Joins components as per design requirements |
| Grinding | Achieves specified dimensions and surface finish |
| Heat treatment | Provides required mechanical properties |
| Painting and coating | Provides specified finish and protection |
| Assembly | Converts individual components into a functional assembly |
| Plastic injection moulding | Produces components in the required shape |
These activities transform the product and contribute to meeting customer requirements.
Example: Automotive component manufacturing
Consider the manufacturing of an automotive bracket.
The process may include:
- Sheet metal cutting.
- Stamping operation.
- Hole punching.
- Welding.
- Surface treatment.
- Final assembly, where applicable.
These operations create the required product characteristics and are generally classified as value-added when performed right first time.
4. What Are Non-Value Added Activities?
A Non-Value Added Activity (NVA) is an activity that consumes time, manpower, material, space or other resources but does not create additional value from the customer’s perspective.
In simple words, customers are not willing to pay for activities that do not improve the product or service.
These activities increase manufacturing costs, production lead time and operational inefficiency.
In Lean Manufacturing, non-value-added activities are commonly associated with waste (Muda).
Examples include:
- Waiting for materials or machine availability.
- Unnecessary transportation of components.
- Excess inventory between processes.
- Rework and repair due to defects.
- Searching for tools and documents.
- Unnecessary movement of operators.
- Duplicate data entry.
- Producing more than customer demand.
Organizations should identify these activities and eliminate them wherever possible.
5. Examples of Non-Value Added Activities
The following examples explain common non-value-added activities in manufacturing.
| Non-value-added activity | Practical manufacturing example |
|---|---|
| Waiting | Components waiting between machining and grinding |
| Transportation | Moving components repeatedly between departments |
| Excess inventory | Keeping more raw material or WIP than required |
| Rework | Re-machining components due to incorrect dimensions |
| Unnecessary motion | Operator walking to collect tools repeatedly |
| Overproduction | Producing more components than customer demand |
| Overprocessing | Performing unnecessary additional operations |
| Searching | Searching for gauges, fixtures or documents |
Practical example: Machining process
Consider an automotive component manufactured through CNC machining.
The operator completes the machining operation, but the components remain in a storage area for two hours before moving to the next process.
During these two hours:
- No additional machining takes place.
- The product characteristics do not improve.
- No additional customer value is created.
- Production lead time increases.
Therefore, the waiting period is a non-value-added activity.
By implementing better production planning, FIFO and improved material flow, the waiting time can be reduced.
6. What Are Necessary Non-Value Added Activities?
Necessary Non-Value Added (NNVA) activities are activities that do not directly add value to the product from the customer’s perspective but are required due to current technical, regulatory, safety or business requirements.
These activities cannot always be eliminated immediately. However, organizations should continuously work to simplify, reduce and optimize them.
Examples of Necessary Non-Value Added Activities
| Activity | Why it may be necessary |
|---|---|
| Incoming material inspection | Verification of purchased material conformity |
| In-process inspection | Monitoring process conformity |
| Final inspection | Verification of finished product requirements |
| Machine setup | Required when changing products or tools |
| Documentation | Maintaining required production and quality records |
| Quality audits | Verification of system and process compliance |
| Statutory testing | Meeting applicable legal requirements |
| Material handling | Moving components between necessary process locations |
Important: Classification depends on the actual process and customer requirements. Inspection does not automatically become value-added simply because it is mandatory. It generally remains non-value-added from the customer’s transformation perspective, although it may be necessary.
Organizations should also consider opportunities to prevent defects at source instead of depending entirely on inspection.
7. Difference Between Value Added, Non-Value Added and Necessary Non-Value Added Activities
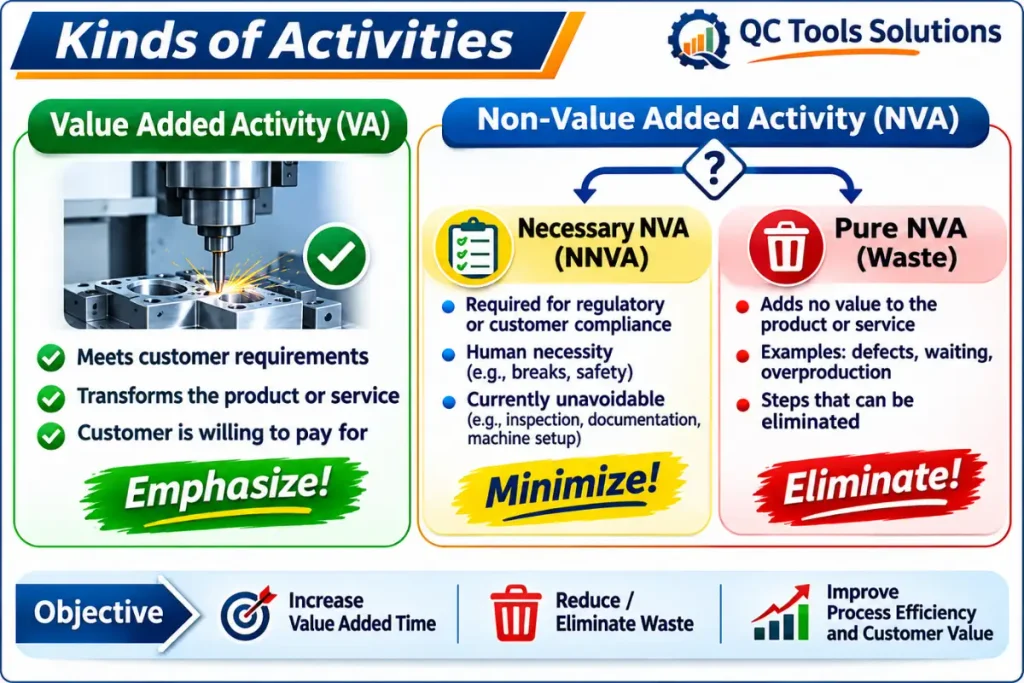
Understanding the difference between these three categories is important for effective Lean Manufacturing implementation.
| Criteria | Value Added (VA) | Non-Value Added (NVA) | Necessary Non-Value Added (NNVA) |
|---|---|---|---|
| Customer value | Creates customer value | Does not create customer value | Does not directly create customer value |
| Customer willingness to pay | Generally yes | No | Generally no |
| Product transformation | Yes | No meaningful transformation | Generally no |
| Necessity | Required to deliver intended product value | Unnecessary waste | Required under current conditions |
| Improvement approach | Improve and optimize | Eliminate | Reduce and simplify |
| Example | Machining | Waiting | Mandatory inspection |
Simple way to remember
- VA: Activities that create customer value.
- NVA: Activities that create waste and should be eliminated.
- NNVA: Activities that are necessary but do not directly create customer value; reduce their time and cost.
8. Value Added vs Non-Value Added Activities in Automotive Manufacturing
Let us understand the classification through practical examples from different automotive manufacturing processes.
A. Stamping Process
In an automotive stamping process, steel sheets are converted into components using stamping presses.
| Activity | Classification |
|---|---|
| Forming sheet metal into the required shape | VA |
| Punching holes as per drawing | VA |
| Waiting for material | NVA |
| Unnecessary movement of sheets | NVA |
| Die changeover | NNVA |
| Required first-off inspection | NNVA |
B. Machining Process
In a machining process, raw material is converted into finished components through different machining operations.
| Activity | Classification |
|---|---|
| Turning to specified dimensions | VA |
| Drilling required holes | VA |
| Grinding to specified tolerance | VA |
| Searching for cutting tools | NVA |
| Rework due to dimensional rejection | NVA |
| Required machine setup | NNVA |
| Mandatory dimensional verification | NNVA |
C. Welding Process
In the welding process, two or more components are joined according to engineering requirements.
| Activity | Classification |
|---|---|
| Welding components | VA |
| Joining brackets as per drawing | VA |
| Waiting for welding fixtures | NVA |
| Excess movement of components | NVA |
| Weld repair due to defects | NVA |
| Required welding parameter verification | NNVA |
D. Painting Process
In the painting process, components receive the specified surface finish and coating.
| Activity | Classification |
|---|---|
| Applying specified coating | VA |
| Achieving required paint thickness | VA |
| Waiting for painting line availability | NVA |
| Excessive movement of components | NVA |
| Repainting due to paint defects | NVA |
| Required curing and verification activities | Depends on the process; curing contributes to the coating result, while verification is generally NNVA |
E. Assembly Process
In an automotive assembly process, different components are assembled to manufacture the final product.
| Activity | Classification |
|---|---|
| Joining components | VA |
| Tightening bolts to specified torque | VA |
| Installing required components | VA |
| Searching for fasteners | NVA |
| Waiting for components | NVA |
| Reassembly due to incorrect fitment | NVA |
| Required torque tool calibration | NNVA |
Note: The classification of an activity should always be evaluated against the customer’s requirements, actual process conditions and the three value-added criteria.
9. Relationship Between Non-Value Added Activities and the 8 Wastes
Non-value-added activities are closely related to the eight wastes of Lean Manufacturing.
The eight wastes are commonly represented by the TIMWOODS concept.
TIMWOODS stands for:
- Transportation
- Inventory
- Motion
- Waiting
- Overproduction
- Overprocessing
- Defects
- Skills (Unused Talent)
Explanation of the 8 Wastes
| Waste | Meaning | Automotive example |
|---|---|---|
| Transportation | Unnecessary movement of materials | Moving components between distant departments |
| Inventory | Excess material or WIP | Excess stock between machining and assembly |
| Motion | Unnecessary movement of people | Operator walking to collect tools |
| Waiting | Idle time | Machine waiting for material |
| Overproduction | Producing more than required | Producing excess components against demand |
| Overprocessing | Performing unnecessary work | Additional finishing not required by specification |
| Defects | Producing defective products | Rejection due to dimensional variation |
| Skills | Underutilization of employee skills | Not involving operators in improvement activities |
How TIMWOODS helps reduce NVA activities
By identifying these eight wastes, manufacturing organizations can understand where time, money and resources are being consumed without creating customer value.
For example:
- Transportation can be reduced through better layout.
- Inventory can be controlled through FIFO and Kanban.
- Motion can be reduced through workplace organization and 5S.
- Waiting can be reduced through improved production planning.
- Overproduction can be controlled through a pull system.
- Overprocessing can be eliminated through process optimization.
- Defects can be reduced through Poka Yoke and process control.
- Unused skills can be addressed through employee involvement and Kaizen.
10. Value Added Time, Non-Value Added Time and Process Cycle Efficiency
Value Added Time (VAT) is the time spent performing activities that directly create customer value.
Non-Value Added Time (NVAT) is the time consumed by activities that do not create customer value.
Total Lead Time is the elapsed time from the beginning of a defined process or order to its completion.
Manufacturing organizations should focus on increasing the proportion of value-added time while reducing unnecessary non-value-added time.
Value Added Ratio Formula
Value Added Ratio (VAR) can be calculated as:
Value Added Ratio = (Value Added Time / Total Lead Time) × 100
Practical Example
Consider an automotive component manufacturing process with the following time distribution:
| Activity | Time | Classification |
|---|---|---|
| CNC machining | 5 minutes | VA |
| Grinding | 4 minutes | VA |
| Assembly | 3 minutes | VA |
| Inspection | 8 minutes | NNVA |
| Material handling | 5 minutes | NNVA |
| Waiting between processes | 25 minutes | NVA |
| Unnecessary movement | 10 minutes | NVA |
| Total lead time | 60 minutes |
Total Value Added Time:
5 + 4 + 3 = 12 minutes.
Total Lead Time = 60 minutes.
Therefore:
VAR = (12 / 60) × 100 = 20%
This means only 20% of the total lead time is spent on value-adding activities.
The remaining 80% is consumed by necessary or unnecessary non-value-added activities.
Improvement Opportunity
Suppose the organization reduces waiting and unnecessary movement through better layout planning and production scheduling.
The new time distribution becomes:
- Value Added Time = 12 minutes.
- Necessary Non-Value Added Time = 13 minutes.
- Unnecessary Non-Value Added Time = 15 minutes.
- Total Lead Time = 40 minutes.
New Value Added Ratio:
VAR = (12 / 40) × 100 = 30%
The value-added ratio increases from 20% to 30%.
Total lead time also reduces from 60 minutes to 40 minutes.
This demonstrates how eliminating unnecessary waste improves manufacturing efficiency without necessarily increasing machine speed or operator workload.
11. How to Identify Non-Value Added Activities
Manufacturing organizations can identify non-value-added activities through systematic process analysis.
The following methods are commonly used.
1. Value Stream Mapping (VSM)
Value Stream Mapping is a Lean tool used to visualize the flow of material and information throughout a process.
It helps identify:
- Process cycle time.
- Waiting time.
- Inventory levels.
- Changeover time.
- Information flow.
- Bottlenecks.
- Value-added and non-value-added time.
VSM helps organizations understand the complete process rather than focusing on individual operations.
2. Process Flow Analysis
Prepare a process flow diagram showing all activities from raw material receipt to finished product dispatch.
Analyze each process step and identify unnecessary operations, repeated activities and delays.
3. Time Study
Conduct a time study to identify the actual time consumed by each activity.
Separate value-added time, necessary non-value-added time and unnecessary non-value-added time.
4. Workplace Observation
Observe operators performing their actual jobs on the shop floor.
Identify activities such as:
- Walking unnecessarily.
- Searching for tools.
- Waiting for material.
- Repeated handling.
- Unnecessary documentation.
- Repeated inspection.
5. Employee Feedback
Involve operators, supervisors and production engineers in identifying process problems.
Employees working directly on the shop floor often know where unnecessary activities occur.
12. How to Eliminate Non-Value-Added Activities
After identifying non-value-added activities, organizations should develop a structured improvement plan.
The following Lean Manufacturing tools can help.
1. 5S
Implement 5S to organize the workplace and reduce unnecessary movement, searching and handling.
2. Kaizen
Encourage employees to identify small improvement opportunities and implement continuous improvements.
3. Poka Yoke
Implement mistake-proofing mechanisms to prevent defects and reduce rework.
4. Kanban
Use a pull-based material replenishment system to control excess inventory and overproduction.
5. Value Stream Mapping
Identify waiting time, excess inventory and process bottlenecks through current-state and future-state mapping.
6. Standardized Work
Establish the best-known method of performing each operation to reduce variation, unnecessary motion and process inefficiency.
7. Layout Improvement
Arrange machines, tools and workstations to minimize unnecessary transportation and operator movement.
8. TPM
Implement Total Productive Maintenance to reduce machine breakdowns and improve equipment availability.
The objective is not simply to make employees work faster. The objective is to remove activities that do not contribute to customer value.
13. Benefits of Reducing Non-Value Added Activities
Reducing non-value-added activities provides several operational and business benefits.
1. Improved Productivity: Employees and machines spend more time on productive activities.
2. Reduced Manufacturing Cost: Unnecessary handling, waiting, rework and inventory costs are reduced.
3. Shorter Lead Time: Removing unnecessary process delays improves delivery performance.
4. Better Product Quality: Reducing rework and preventing defects improves process consistency.
5. Improved Resource Utilization: Manpower, machines, materials and production space are utilized more effectively.
6. Increased Customer Satisfaction: Better quality, shorter delivery time and competitive costs improve customer satisfaction.
7. Continuous Improvement: Employee involvement in identifying and eliminating waste supports a continuous improvement culture.
14. Application in ISO 9001 and IATF 16949
The concepts of value-added and non-value-added activities support process efficiency, risk-based thinking and continual improvement in quality management systems.
Manufacturing organizations implementing ISO 9001 and IATF 16949 can use Lean Manufacturing techniques to improve their processes.
Some relevant areas include:
- Process approach and process effectiveness.
- Operational planning and control.
- Risk-based thinking.
- Monitoring and measurement of processes.
- Control of nonconforming outputs.
- Corrective action.
- Continual improvement.
Organizations can use process analysis, Value Stream Mapping, Kaizen, Poka Yoke and other Lean tools to identify improvement opportunities.
The objective is to ensure that processes consistently meet customer requirements while minimizing waste and unnecessary resource consumption.
15. Frequently Asked Questions (FAQs)
Q1. What are value-added activities in manufacturing?
Value-added activities are operations that transform a product according to customer requirements and create customer value. Examples include machining, stamping, welding, painting, heat treatment and assembly.
Q2. What are non-value-added activities?
Non-value-added activities consume time, manpower or resources without creating additional customer value. Examples include waiting, unnecessary transportation, excess inventory, rework and unnecessary movement.
Q3. What is the difference between value-added and non-value-added activities?
Value-added activities transform a product or service in a way that the customer values. Non-value-added activities consume resources without increasing customer value. Organizations should maximize value-added activities and eliminate unnecessary non-value-added activities.
Q4. What are necessary non-value-added activities?
Necessary non-value-added activities are activities that do not directly create customer value but are required due to technical, statutory, regulatory, safety or business requirements.
Examples include mandatory inspection, required documentation, machine setup and quality audits.
Q5. Is inspection a value-added or non-value-added activity?
Inspection is generally classified as non-value-added because it verifies product conformity but does not transform the product. However, inspection may be necessary to meet customer, safety or regulatory requirements. Therefore, it is commonly classified as necessary non-value-added.
Q6. What are the three criteria of a value-added activity?
The three criteria are:
- The customer must be willing to pay for the activity.
- The activity must transform the product or service.
- The activity must be performed correctly the first time.
Q7. What are examples of value-added activities in automotive manufacturing?
Examples include sheet metal stamping, CNC machining, welding, grinding, painting, heat treatment and assembly when these operations fulfil customer requirements.
Q8. What are examples of non-value-added activities in automotive manufacturing?
Examples include waiting for materials, unnecessary transportation, excess WIP inventory, searching for tools, rework due to defects and unnecessary operator movement.
Q9. How can non-value-added activities be eliminated?
Organizations can use Lean tools such as 5S, Kaizen, Value Stream Mapping, Kanban, Poka Yoke, TPM and standardized work to identify and reduce unnecessary activities.
Q10. What is the relationship between non-value-added activities and the 8 wastes?
The eight wastes of Lean Manufacturing represent common forms of non-value-added activities. They include Transportation, Inventory, Motion, Waiting, Overproduction, Overprocessing, Defects and Unused Skills.
Q11. How do you calculate the value-added ratio?
Value Added Ratio is calculated by dividing Value Added Time by Total Lead Time and multiplying the result by 100.
For example, if value-added time is 12 minutes and total lead time is 60 minutes, the value-added ratio is 20%.
Q12. What is the difference between value-added time and lead time?
Value-added time is the time spent performing activities that create customer value. Lead time is the total elapsed time required to complete a process or order, including processing, waiting and other activities.
16. Conclusion
Understanding the difference between value-added and non-value-added activities is essential for implementing Lean Manufacturing and improving operational efficiency.
Manufacturing organizations should focus on identifying activities that create customer value and eliminating unnecessary activities that consume time, money and resources.
Value-added activities such as machining, stamping, welding, painting and assembly contribute directly to product transformation.
Non-value-added activities such as waiting, excess inventory, unnecessary transportation and rework should be systematically reduced or eliminated.
Necessary non-value-added activities, such as mandatory inspection and documentation, should be simplified and optimized wherever possible.
By applying Lean Manufacturing tools such as 5S, Kaizen, Value Stream Mapping, Kanban, Poka Yoke and TPM, organizations can improve productivity, reduce manufacturing costs, shorten lead time and achieve operational excellence.
Remember: The objective of Lean Manufacturing is not to keep everyone busy. It is to create maximum customer value with minimum waste.
About QC Tools Solutions
QC Tools Solutions provides practical learning resources, training and consultancy support in Quality Management Systems, ISO 9001, IATF 16949, Lean Manufacturing, Core Tools and process improvement.
Visit QC Tools Solutions for more quality management and manufacturing improvement resources.
Real clean web site, appreciate it for this post.